What Causes Water Hammer in Steam Systems? 7 Common Causes and How to Prevent It
What Causes Water Hammer in a Steam System?
Water hammer in a steam system usually occurs when condensate accumulates in piping or equipment and is suddenly accelerated by steam, or when pockets of steam rapidly condense and surrounding condensate rushes into the resulting space.
Common contributing conditions include poor condensate drainage, incorrectly sloped piping, malfunctioning or misapplied steam traps, rapid startup, equipment stall, condensate collecting in dead legs, and problems within condensate-return piping.
Water hammer should never be treated as normal steam-system noise. The impact can place significant mechanical stress on piping, valves, supports, steam traps, and connected equipment.
The correct solution starts with identifying where condensate is accumulating and why.
At Colton Industries, steam-system reliability is approached as a system issue. Components such as steam traps, strainers, check valves, and other pipeline specialties all play a role in controlling flow and helping condensate move where it should. Colton has supplied industrial and commercial flow-control equipment across North America since 1988.
What Is Water Hammer in a Steam System?
Water hammer is a hydraulic shock that occurs when liquid inside a piping system changes velocity rapidly or when steam suddenly condenses in the presence of condensate.
In steam systems, two important mechanisms can produce water hammer.
Condensate-Induced Water Hammer
Condensate collects inside steam piping and forms a slug of water.
High-velocity steam can push that condensate through the pipe until it strikes:
- An elbow
- Valve
- Tee
- Pipe fitting
- Closed end
- Other obstruction
Because liquid is much denser than steam, the resulting impact can create a powerful mechanical shock.
Steam-Induced Water Hammer
Another form occurs when a pocket of steam becomes trapped between areas of cooler condensate.
The steam can condense very rapidly. As its volume collapses, condensate rushes toward the resulting low-pressure area and collides.
TLV identifies both high-speed condensate impact and the sudden condensation of steam as mechanisms that can produce water hammer.
The important takeaway is:
Water hammer is not simply “steam moving too fast.” It is closely tied to the presence and behavior of condensate.
What Are the Signs of Water Hammer?
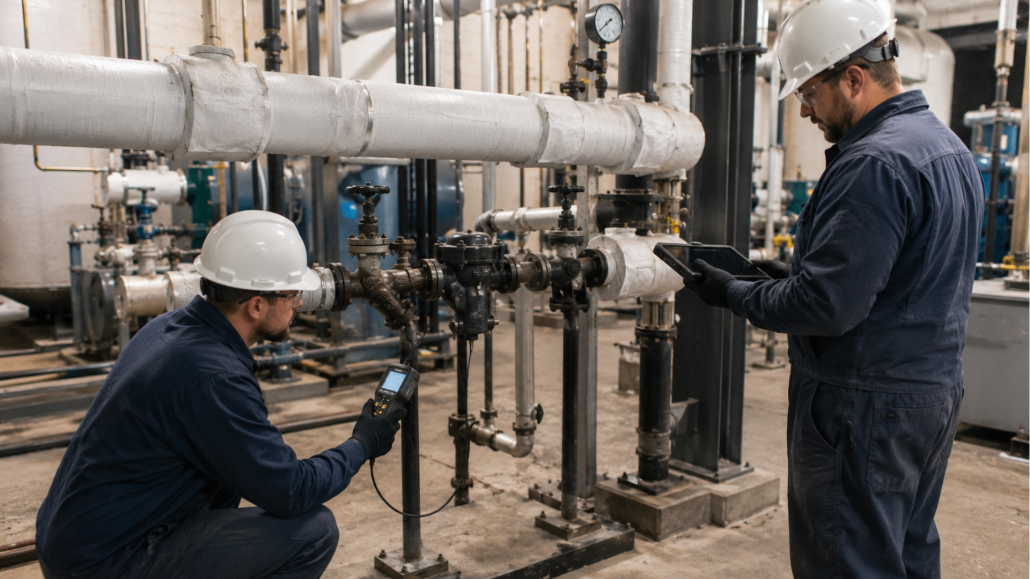
Maintenance technicians inspect steam traps, valves, strainers, and condensate drainage conditions while troubleshooting water hammer.
Water hammer can sound different depending on the system and severity.
Possible warning signs include:
- Banging or hammering inside piping
- Sharp metallic impacts
- Pipe movement
- Shaking or vibration
- Repeated knocking during startup
- Noise near steam traps or valves
- Sudden movement of pipe supports
- Unusual noise in condensate-return lines
Severe water hammer may also contribute to:
- Damaged valves
- Failed pipe supports
- Leaking joints
- Damaged steam traps
- Piping deterioration
- Equipment damage
Any recurring hammering should be investigated rather than accepted as a normal part of startup.
What Are the Most Common Causes of Water Hammer in Steam Systems?
These seven conditions should be among the first areas maintenance teams investigate.
1. Condensate Is Accumulating in Steam Piping
One of the most common underlying conditions behind steam-system water hammer is condensate that is not being removed effectively.
Steam naturally forms condensate as it loses heat.
This occurs during normal operation, but condensate production can be especially high when:
- Steam enters cold piping
- The system starts after a shutdown
- Outdoor temperatures drop
- Insulation is missing or damaged
- Steam demand changes rapidly
If condensate remains in the line, flowing steam can push it forward.
The resulting slug of water can strike fittings, valves, or changes in pipe direction with significant force.
Can condensate cause water hammer?
Yes. Condensate accumulation is a major contributor to water hammer in steam distribution systems. Effective drainage is one of the most important elements of water-hammer prevention.
TLV specifically recommends rapidly and completely removing condensate from steam distribution lines as a primary measure for controlling water hammer.
2. Steam Traps Are Not Removing Condensate Properly
Steam traps are responsible for removing condensate and non-condensable gases while limiting the loss of live steam.
When a trap:
- Fails closed
- Becomes blocked
- Is undersized
- Is incorrectly selected
- Is installed improperly
- Cannot overcome downstream pressure
condensate may remain upstream.
Can a bad steam trap cause water hammer?
Yes. A malfunctioning or improperly applied steam trap can contribute to water hammer when it prevents condensate from draining effectively.
However, the presence of water hammer does not automatically prove that a steam trap has failed.
The trap may be operating correctly while another condition prevents condensate from reaching or leaving it.
Maintenance teams should examine:
- Trap operation
- Trap selection
- Differential pressure
- Upstream strainer condition
- Downstream backpressure
- Piping slope
- Drainage arrangement
Colton offers several types of industrial steam traps, including float and thermostatic, balanced-pressure thermostatic, thermodynamic, inverted-bucket, and bi-metal configurations.
The correct trap depends on the application and operating conditions, not simply the pipe size.
3. Steam Piping Is Sloped Incorrectly
Even functioning steam traps cannot drain condensate properly if the piping does not allow condensate to reach the drainage point.
Steam distribution piping should be designed so condensate travels toward appropriate drip and trap locations.
Incorrect slope can create low points where water accumulates.
TLV notes that if properly located steam traps are present but water hammer continues, incorrect piping slope may be a cause because condensate cannot reach the trap as intended. Even relatively small unintended rises in long steam lines can create problematic accumulation points.
Can incorrect pipe slope cause water hammer?
Yes. Improper steam-main slope can allow condensate to pool in locations that are not adequately drained, increasing the risk of water hammer.
This is why persistent water hammer should sometimes trigger a piping review rather than repeated component replacement.
4. Steam Is Introduced Too Quickly During Startup
Cold piping generates a large amount of condensate as steam first enters the system.
Opening the steam supply too quickly can create two problems:
- Condensate is generated rapidly.
- Steam velocity can move accumulated condensate through the piping before it drains.
Gradually opening the steam supply helps the system warm more evenly and can reduce the force associated with rapidly moving condensate.
TLV recommends slowly operating steam valves during startup as one measure that can reduce water hammer caused by high-speed condensate.
Why does water hammer often happen during startup?
Water hammer is common during startup because cold steam piping initially produces large amounts of condensate. If steam is introduced faster than condensate can drain, water can accumulate and be accelerated through the piping.
A controlled warm-up allows:
- Piping temperature to rise gradually
- Air to escape
- Condensate to drain
- Steam pressure to stabilize
Facility startup procedures should always follow applicable engineering and equipment requirements.
5. Equipment Is Experiencing Stall
Water hammer does not occur only in steam mains.
It can also develop inside steam-using equipment such as heat exchangers.
A condition known as stall can occur when the pressure available upstream of the steam trap is no longer sufficient to overcome downstream condensate-return pressure.
When that happens, condensate cannot drain properly even though the trap itself may be functioning.
This can occur when:
- Process load falls
- A control valve throttles steam pressure
- Condensate-return pressure remains elevated
- Equipment shuts down
- Steam pressure inside the equipment decreases
Condensate can then accumulate inside the equipment.
When steam interacts with the accumulated condensate, water hammer can occur.
TLV specifically identifies accumulated condensate associated with stall as a source of water hammer in steam-using equipment.
Can a working steam trap still have drainage problems?
Yes. A steam trap needs sufficient differential pressure to discharge condensate. A mechanically functional trap may not drain properly if system pressure conditions prevent flow.
This is an important reason not to automatically blame the trap whenever equipment floods.
6. Condensate Is Collecting in Dead Legs or Poorly Drained Branches
Condensate can collect anywhere piping creates a location that is difficult to drain.
Problem areas may include:
- Dead-ended branch lines
- Low points
- Improperly pitched branches
- Sections left after system modifications
- Inactive steam lines connected to active mains
- Poorly positioned trap stations
TLV identifies condensate accumulation in dead-ended branch piping as another possible contributor to water hammer.
These locations can be particularly difficult to identify because the nearest steam trap may be functioning normally.
When water hammer repeatedly occurs in the same section of a system, review the physical piping configuration, not just individual components.
7. Steam and Condensate Are Interacting in the Condensate Return System
Water hammer can also occur after the condensate leaves the steam trap.
Condensate-return piping can contain a mixture of:
- Hot condensate
- Cooler condensate
- Flash steam
Under certain conditions, steam pockets can collapse rapidly when they contact cooler condensate.
This can create steam-induced water hammer inside the return system.
TLV notes that condensate-return piping is inherently susceptible to this phenomenon because high-temperature flash steam and lower-temperature condensate may coexist in the same piping.
Can water hammer occur in condensate return piping?
Yes. Water hammer can occur in condensate-return lines when steam or flash-steam pockets rapidly condense in the presence of cooler condensate.
Troubleshooting this type of hammer requires looking beyond the steam trap itself.
Can a Clogged Strainer Contribute to Water Hammer?
Indirectly, yes.
An upstream strainer helps protect steam traps, valves, and other equipment from debris.
If a strainer becomes heavily clogged, the resulting restriction can affect pressure and flow available to downstream components.
In a steam-trap station, severe restriction may interfere with effective condensate drainage.
That does not mean every clogged strainer will cause water hammer.
However, when troubleshooting poor trap performance or condensate accumulation, the upstream strainer should be checked.
Colton’s industrial strainer portfolio includes Y-strainers, basket strainers, duplex basket strainers, replacement screens, and temporary strainers.
How Do You Stop Water Hammer in a Steam System?
There is no single fix for every water-hammer problem.
The correct solution depends on where the hammer occurs and what is allowing condensate or steam pockets to develop.
A systematic approach should include the following.
1. Find Where Condensate Is Accumulating
Do not begin by replacing random components.
Identify:
- Where the noise occurs
- When it happens
- Whether it occurs only during startup
- Whether it continues during steady operation
- Whether closing steam stops the hammer
- Whether the problem is in steam piping, equipment, or condensate return
These clues can help distinguish different water-hammer mechanisms.
2. Verify Steam Trap Operation
Inspect traps in the affected area for:
- Blockage
- Incorrect operation
- Improper selection
- Insufficient capacity
- Installation problems
- Inadequate differential pressure
Review Colton’s steam trap solutions when evaluating whether the existing trap remains appropriate for the application.
3. Inspect Strainers
Check upstream strainers for:
- Debris accumulation
- Damaged screens
- Restricted flow
- Incorrect installation orientation
A clean and correctly selected strainer helps protect downstream steam-system components.
4. Verify Pipe Slope and Drainage
Look for:
- Sagging pipe
- Improper slope
- Unsupported sections
- Undrained low points
- Dead legs
- Long horizontal runs without adequate drainage
TLV emphasizes that a survey of the entire piping system may be necessary to identify the actual cause of persistent water hammer.
5. Review Startup Procedures
If hammer occurs primarily at startup:
- Introduce steam gradually
- Allow piping to warm
- Confirm drainage before increasing flow
- Monitor trap operation
- Listen for abnormal noise before reaching full operating pressure
6. Check Condensate Return Pressure
If equipment is flooding despite a functioning trap, investigate whether sufficient differential pressure exists.
The issue may involve:
- Return-line backpressure
- Equipment stall
- Trap selection
- Return-system design
7. Investigate the Entire System
Water hammer is often a system problem rather than a single-component problem.
A trap, valve, or strainer may be involved, but replacing one component without identifying the actual mechanism may leave the problem unresolved.
How Can You Prevent Water Hammer?
Preventive maintenance should focus heavily on reliable condensate removal.
Keep Steam Traps Operating Properly
Establish a steam trap testing program and investigate failed or repeatedly problematic traps.
Keep Strainers Clean
Inspect strainers based on actual system debris load and clean them before restriction becomes excessive.
Maintain Proper Drainage
Verify:
- Drip legs
- Low points
- Steam-main slope
- Trap locations
- Branch drainage
Start Steam Systems Gradually
Avoid unnecessarily rapid pressurization of cold steam lines.
Investigate Repeat Problems
If the same area repeatedly experiences hammer, determine why.
Repeated symptoms can indicate:
- Incorrect piping
- Poor drainage
- Trap misapplication
- Equipment stall
- Return-system problems
Maintain Related Flow-Control Components
Inspect:
- Valves
- Check valves
- Pressure-reducing equipment
- Flexible connectors
- Pipe supports
- Condensate-return components
Colton Industries supplies a broad portfolio of steam and pipeline flow-control products for industrial and commercial systems, including steam traps, strainers, check valves, flexible connectors, pressure-reducing valves, and related pipeline specialties.
What Should You Check When Troubleshooting Water Hammer?
Use this practical troubleshooting checklist.
Steam Traps
- Are traps discharging condensate?
- Are any traps blocked?
- Is the trap properly sized?
- Is the trap type appropriate?
- Is adequate differential pressure available?
Strainers
- Are screens clogged?
- Is pressure drop excessive?
- Is the Y-strainer installed correctly?
- Is debris repeatedly accumulating?
Steam Mains
- Is the pipe correctly sloped?
- Are low points properly drained?
- Are drip legs positioned correctly?
- Are there undrained dead legs?
- Is piping sagging?
Valves and Startup
- Is steam being introduced too quickly?
- Are isolation valves fully open?
- Are control valves operating correctly?
- Are pressure conditions stable?
Equipment
- Is condensate backing up?
- Does hammer occur during low load?
- Could the equipment be stalling?
- Has the process operating condition changed?
Condensate Return
- Is backpressure excessive?
- Are check valves functioning?
- Is flash steam interacting with cooler condensate?
- Does hammer continue after the steam supply is isolated?
The objective is to move from:
Noise → location → mechanism → root cause → corrective action.
Is Water Hammer Dangerous?
Yes. Water hammer can generate significant mechanical forces inside piping systems.
Potential consequences include damage to:
- Piping
- Valves
- Fittings
- Pipe supports
- Steam traps
- Connected equipment
TLV documents that condensate slugs striking piping components and sudden steam condensation can both generate powerful impacts.
Recurring water hammer should therefore be treated as a maintenance and reliability problem, not simply an annoyance.
Frequently Asked Questions About Steam-System Water Hammer
What causes water hammer in steam systems?
Water hammer is commonly caused when condensate accumulates in steam piping and is accelerated by steam, or when trapped steam rapidly condenses and surrounding condensate rushes together. Poor drainage, trap problems, incorrect pipe slope, rapid startup, equipment stall, and condensate-return conditions can all contribute.
Can a bad steam trap cause water hammer?
Yes. A blocked, failed, undersized, misapplied, or improperly operating steam trap can contribute to condensate accumulation and water hammer. However, trap failure is only one possible cause.
Can condensate cause water hammer?
Yes. Accumulated condensate is central to many forms of steam-system water hammer. High-speed steam can accelerate condensate slugs through piping, while rapid steam condensation can cause surrounding condensate to collide.
How do you stop water hammer in a steam line?
Start by identifying where condensate is accumulating. Check steam traps, strainers, piping slope, drainage points, startup procedures, differential pressure, and condensate-return conditions. Persistent problems may require reviewing the entire piping system.
Does opening a steam valve too quickly cause water hammer?
It can. Rapidly introducing steam into cold piping can generate condensate quickly and accelerate accumulated water. Gradual startup can reduce some forms of condensate-induced water hammer.
Can water hammer occur even when the steam trap works?
Yes. Incorrect piping slope, equipment stall, excessive return pressure, dead legs, rapid startup, or condensate-return problems can cause water hammer even when an individual trap is mechanically functional.
Can water hammer happen in condensate return piping?
Yes. Flash steam and cooler condensate can interact in condensate-return piping, allowing steam pockets to collapse rapidly and produce water hammer.
Do Not Treat Water Hammer as a Single-Component Problem
One of the biggest troubleshooting mistakes is assuming that every hammering steam line needs a new steam trap.
A failed trap may be involved.
But the root cause could instead be:
- Incorrect piping slope
- A clogged strainer
- Excessive backpressure
- Equipment stall
- An undrained dead leg
- Improper startup
- Condensate-return conditions
Replacing a functioning component will not correct an underlying system problem.
The stronger approach is to evaluate the full path:
Steam supply → piping → drainage → steam trap → condensate return
At Colton Industries, that system-level perspective is important. Colton is a family-owned North American manufacturer and supplier whose portfolio includes steam traps, strainers, check valves, flexible connectors, pressure-reducing valves, and related pipeline flow-control equipment.
Final Takeaway
So, what causes water hammer in a steam system?
The seven common causes to investigate are:
- Condensate accumulation in steam piping
- Steam traps that are not removing condensate effectively
- Incorrect piping slope
- Steam being introduced too quickly during startup
- Equipment stall
- Poorly drained dead legs or branches
- Steam and condensate interaction in return piping
The common thread is condensate control.
When water hammer occurs, do not simply silence the symptom or replace the nearest component.
Find out:
Where is condensate accumulating? Why is it accumulating? What is preventing it from draining correctly?
That approach leads to better troubleshooting and more reliable corrective action.
Explore Colton Industries’ steam and pipeline product solutions or contact the Colton team to discuss steam traps, strainers, valves, and related components for your system.
